
Second low-pressure die casting furnace, fully relined
Not patched, but completely broken out and rebuilt
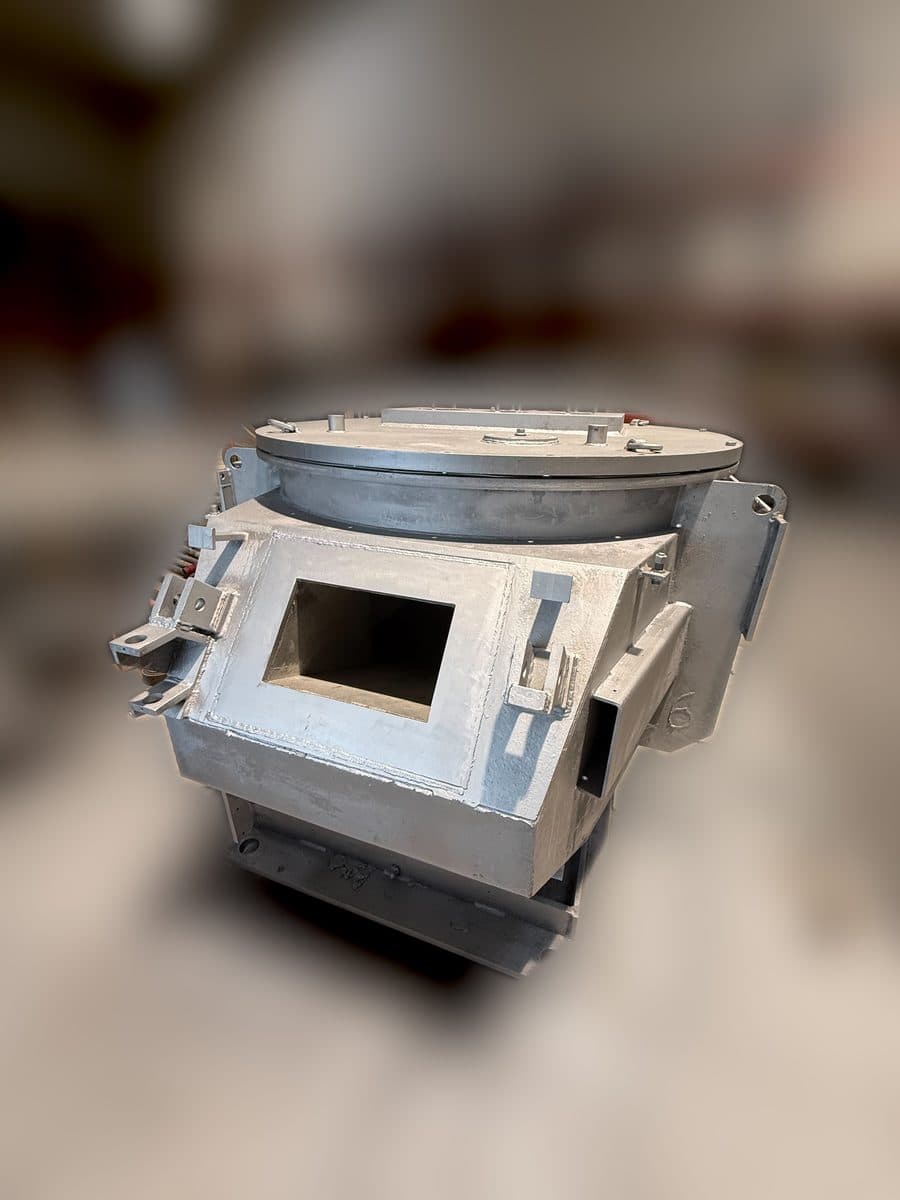
Initial situation
After the general overhaul of a low-pressure die casting furnace in the summer, a second furnace of this type arrived at the SBS Refractory Service workshop in November, from a different customer and in considerably worse condition. The casing was encrusted and rusty, and the old brick lining had broken out in many places. A low-pressure die casting furnace is a closed furnace that works with gas pressure: a gas overpressure above the aluminium bath pushes the melt through the riser tube into the die. A lining that only holds in places cannot be sensibly patched for this duty. The decision was therefore taken to reline the furnace completely.
Scope of services
- Complete relining
- Break-out
- Castable
- Insulating firebricks
- Two-component castable
- Workshop repair
Project data
The task
With an old lining in this condition, there is no telling what is still sound behind the visible layer. New material placed on crumbling insulation does not last long.
The bath chamber is round and has several wall openings as well as a charging opening at the front. Bricked, this would mean many joints and cut-to-fit pieces where aluminium attacks.
The floor carries the load of the bath and takes the greatest mechanical wear during cleaning.
After relining, the lid and sealing faces must close gas-tight again, otherwise the furnace cannot hold the pressure.
The SBS approach
The old lining was broken out completely. This gave free access to the steel casing, and no remnants of old, embrittled insulation were left in the new build-up.
The walls of the bath chamber were cast monolithically in formwork, including the wall openings. A cast wall has no brick joints for the melt to penetrate.
Insulating firebricks were installed behind the cast wall over its full height; they can be seen as a ring at the upper edge of the bath chamber. They reduce heat losses and lower the casing temperature.
The floor was cast with a special two-component castable. The two components are only mixed on site in the specified ratio and produce a dense, load-bearing floor.
Finally, the casing was painted and the lid with its penetrations was refurbished. The first heat-up follows a curve with holding stages so that the water in the fresh castable escapes in a controlled way. The customer carries out the tightness test itself before commissioning.
Second low-pressure die casting furnace, fully relined in pictures
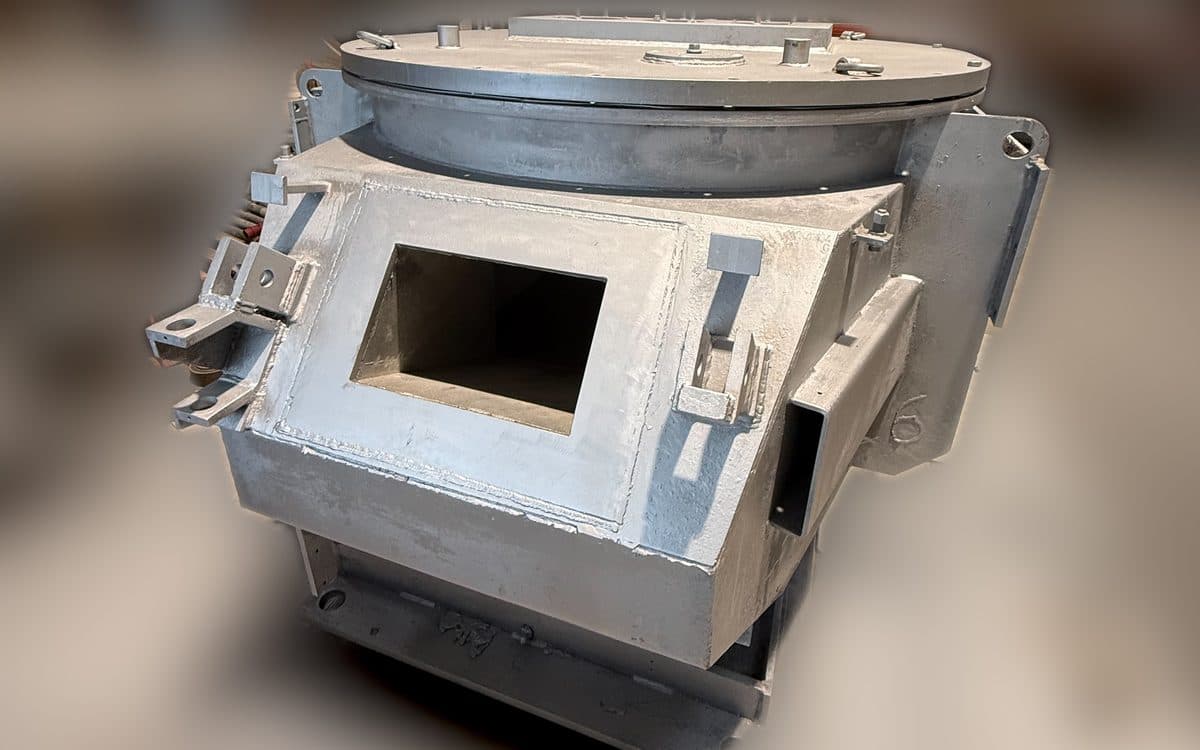
Finished: relined, casing painted, lid fitted
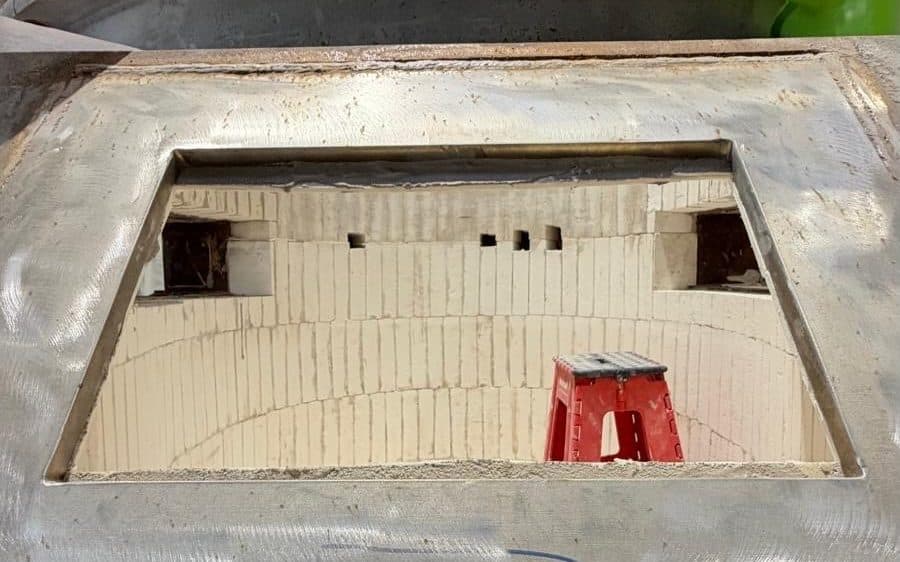
On delivery: old lining broken out in many places
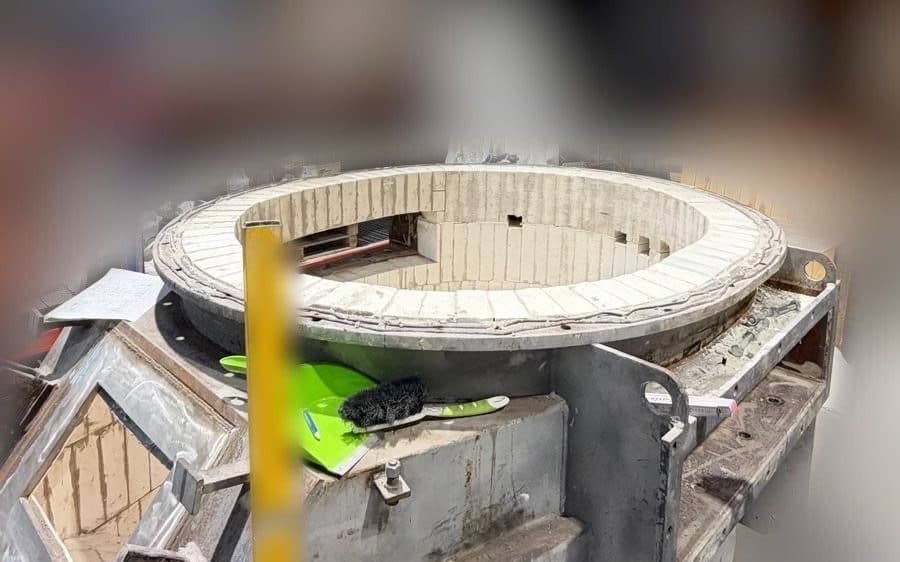
Upper edge of the old brick lining before break-out
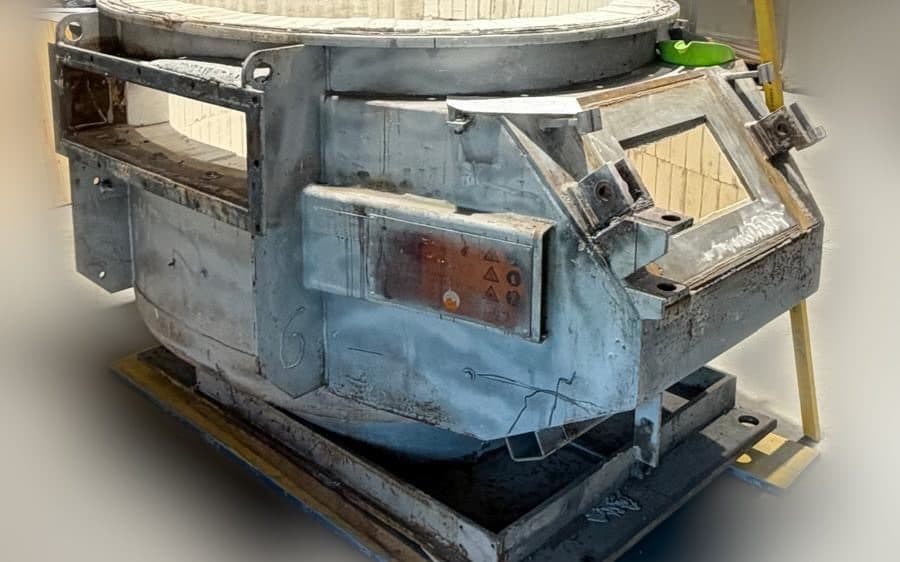
The casing in its original condition
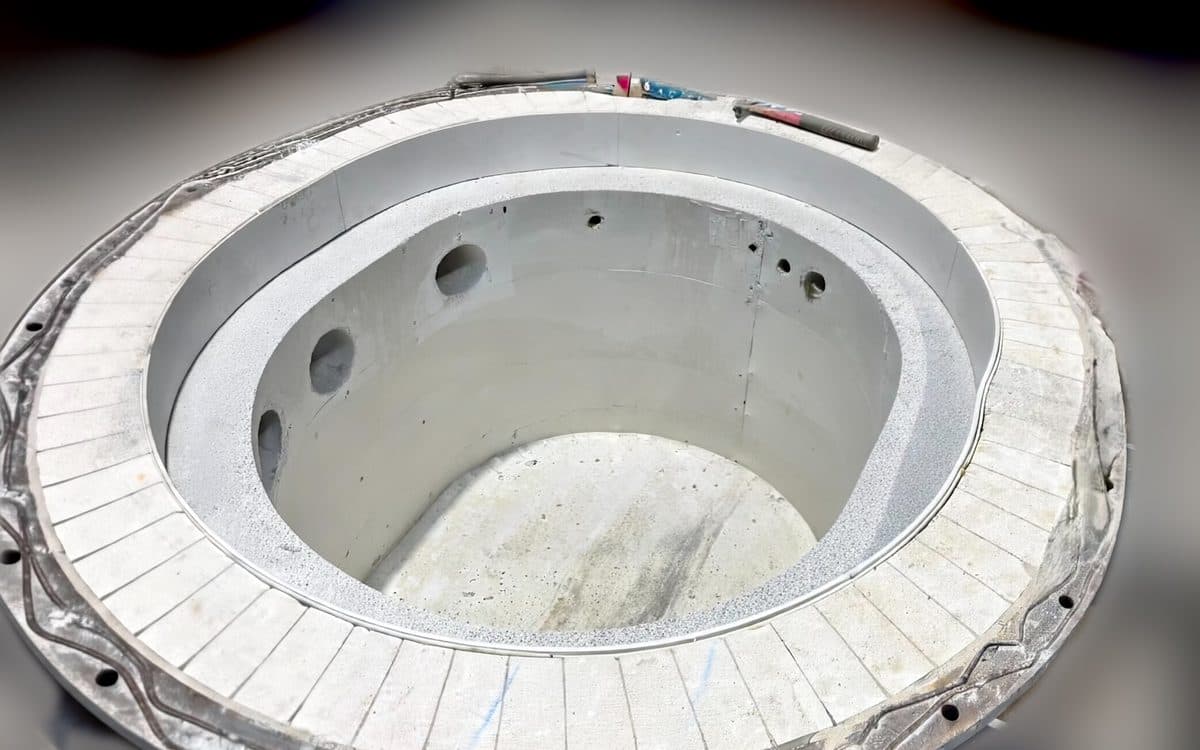
New bath chamber: cast walls, insulating firebricks at the upper edge
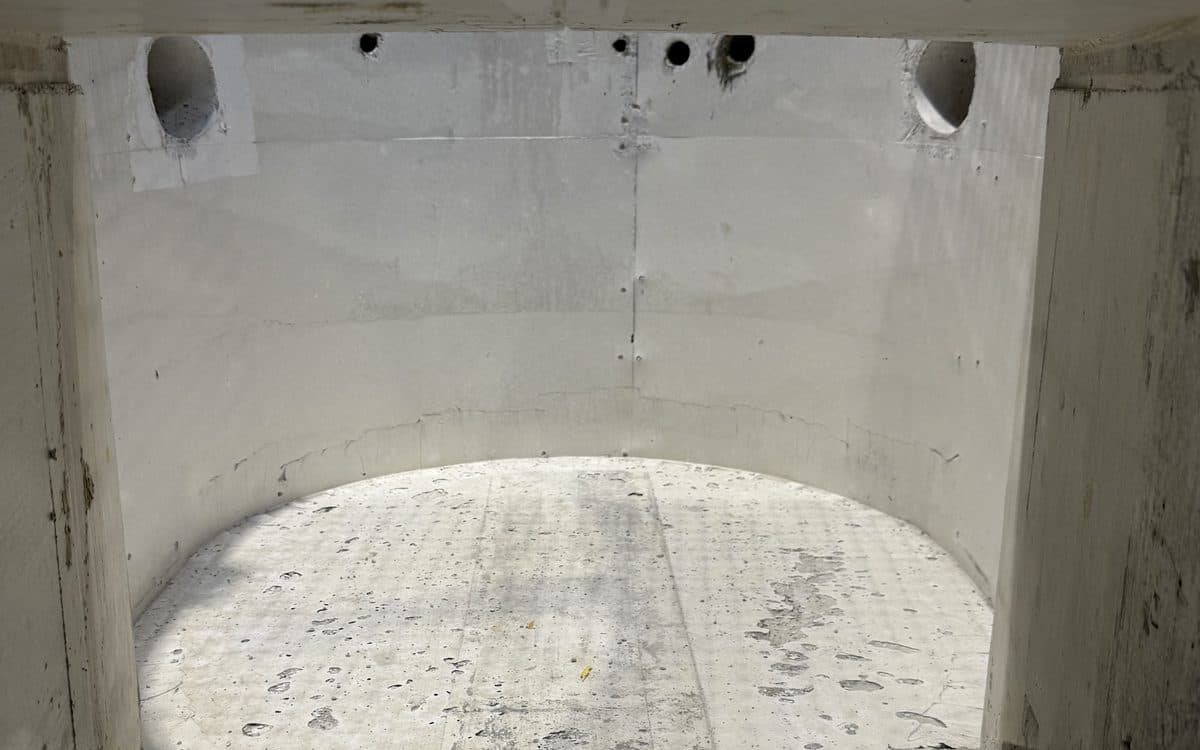
Cast wall and floor in two-component castable
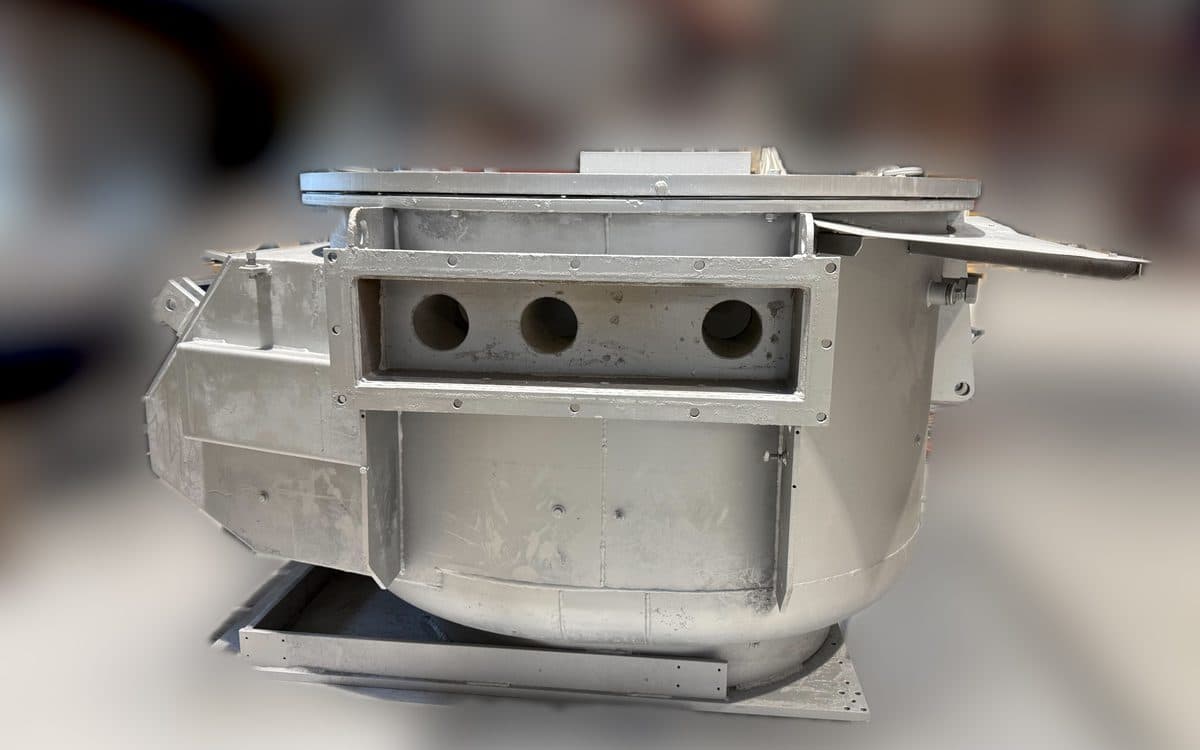
Side view after relining
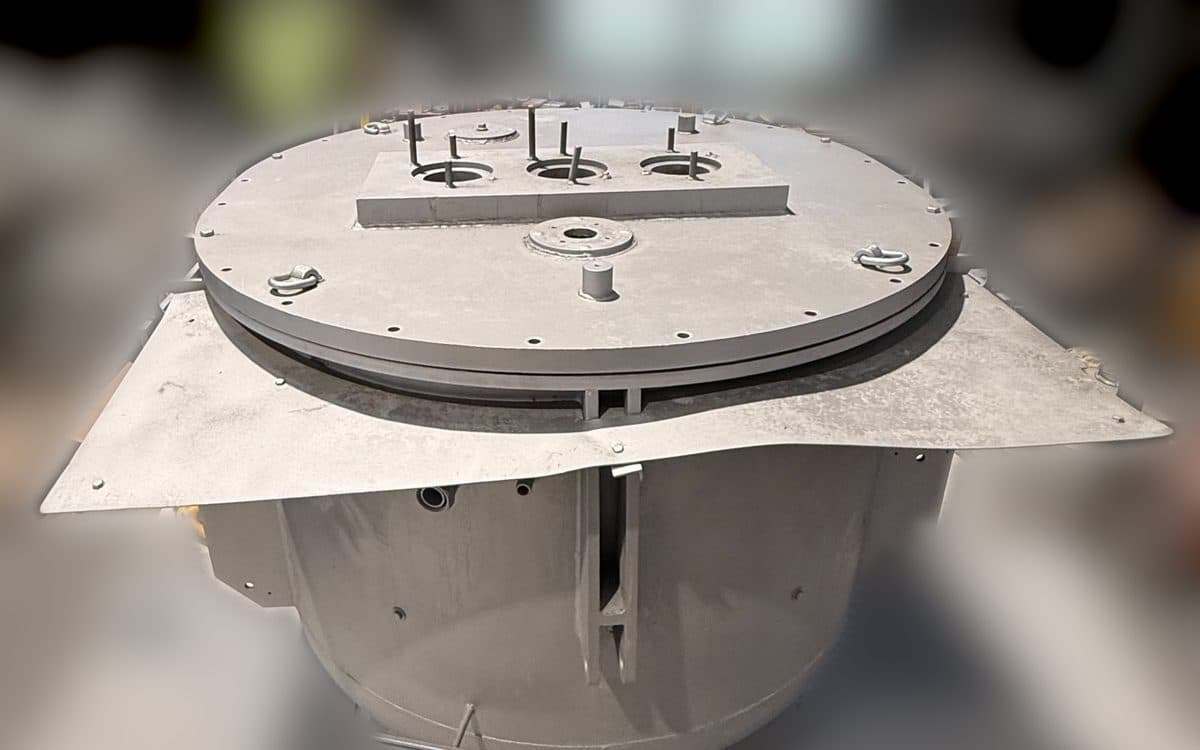
Lid with penetrations, ready for return
Measurable results
The key figures of the “Second low-pressure die casting furnace, fully relined” project
Similar references
A similar project at your site?
We look at your plant and tell you what is possible: partial repair, relining or maintenance during operation. Free initial consultation, quick reply.